


Table of Contents
You've decided robotic welding is the right direction for your factory. Now you're looking at configurations and seeing terms like "open workstation," "enclosed workstation," "mobile welding station," and "welding cell" — sometimes used interchangeably, sometimes meaning very different things. This guide cuts through the confusion and gives you a clear, practical understanding of what a robotic welding workstation actually is, what the different configurations mean, and which one fits your specific production environment.
A robotic welding workstation is not just a robot arm with a welding torch attached. It is a complete, integrated production system — and the configuration choices you make around the robot itself are just as important as the robot and welding process selection. Getting the workstation configuration right from the start determines how safely your operators work, how efficiently your production runs, how cleanly your workshop environment stays, and how quickly you can deploy and adapt the system as your production needs evolve.

What Is a Robotic Welding Workstation?
A robotic welding workstation is a complete, integrated system that combines a robotic arm, welding process equipment, workpiece fixturing, and supporting infrastructure into a single production unit designed for automated, repeatable welding.
The key word is integrated. A robotic welding workstation is not simply a robot arm positioned near a welding table — it is a purposefully designed system where every component is selected and configured to work together for a specific production application.
The Core Components of Any Robotic Welding Workstation
Regardless of configuration type, every robotic welding workstation includes some combination of the following:
1. The Robot ArmThe robotic arm provides programmable, repeatable movement along the welding path. This may be a 6-axis collaborative robot (cobot) for flexible, human-proximate operation, or a 6-axis industrial robot for high-speed, high-payload applications. DATO workstations are configured with proven robot platforms including the Aubo i10 6-axis collaborative robot for cobot applications and the LA1813-25 industrial 6-axis robot for heavy-duty industrial welding.
2. The Welding Process EquipmentThe welding power source and welding head — whether a fiber laser source with automatic laser welding head, a TIG welding power source, or a MIG/MAG welding system — deliver the actual welding energy. The choice of welding process is independent of the workstation configuration type; the same open or enclosed structure can house laser welding, TIG welding, or MIG welding equipment.
3. The Wire Feeding SystemFor welding processes that use filler wire, an automated wire feeding system delivers wire at a controlled, consistent rate. Wire diameter options (0.8 / 1.0 / 1.2 / 1.6mm) are selected based on material, joint design, and welding parameters.
4. The Workpiece Fixture and Welding Table / PositionerThe fixture holds the workpiece in the correct position and orientation for the robot to execute its programmed welding path. This may be a simple flat welding platform, a single-axis rotary positioner, a dual-axis P-type positioner, or a headstock-tailstock positioner for long or complex parts. Fixture design is one of the most critical factors in workstation performance — poor fixturing is the most common cause of inconsistent weld quality in robotic welding.
5. The Control SystemThe control system manages robot movement, welding parameters, wire feeding, and production programs. Modern robotic welding control systems support programmable welding paths, parameter storage for multiple part programs, and integration with factory production management systems.
6. Safety and Environmental InfrastructureThis is where open and enclosed configurations diverge most significantly — and where the configuration choice has the most direct impact on operator safety, workshop environment, and regulatory compliance.
7. Optional UpgradesDepending on the application and production requirements: smoke purifier, gun cleaning system, wire cutting system, safety light curtains, and automation integration options.

The Two Primary Configuration Types: Open vs Enclosed
The most fundamental configuration choice in robotic welding workstation design is whether the system operates in an open or enclosed structure. This single decision affects safety, cost, floor space, operator workflow, environmental compliance, and deployment flexibility more than almost any other configuration choice.
Open Robotic Welding Workstation
What It Is
An open robotic welding workstation operates without a full physical enclosure around the robot and welding zone. The robot arm, welding head, and workpiece are accessible from the surrounding workshop floor. Safety is managed through a combination of the cobot's built-in safety features (force/torque sensing, speed limiting, collision detection), safety light curtains, area scanners, and defined operator exclusion zones — rather than through physical walls.
For laser welding specifically, even open workstations require a controlled laser safety zone, appropriate laser safety interlocks, and operator eye protection — because the laser itself is a Class 4 hazard regardless of the robot type. The "open" designation refers to the absence of a full physical enclosure, not the absence of safety measures.
Key Advantages of Open Configuration
Maximum Loading and Unloading FlexibilityWithout physical walls constraining access, operators can load and unload workpieces from any direction. This is particularly valuable for large, awkward, or heavy parts that are difficult to maneuver through an enclosure door. It also allows the use of overhead cranes, forklifts, or other material handling equipment without spatial constraints.
Lower Initial InvestmentOpen workstations eliminate the cost of the enclosure structure itself — which can represent a meaningful portion of the total system cost, particularly for larger workstations. For manufacturers where budget is a primary constraint and the workshop environment and safety requirements allow open operation, this is a genuine financial advantage.
Faster Deployment and ReconfigurationWithout an enclosure to install, align, and integrate, open workstations can be deployed faster. They are also easier to reconfigure — moving the workstation to a different location, changing the fixture layout, or modifying the robot's working area involves fewer constraints.
Better Visibility for Operators and SupervisorsOpen workstations allow operators and production supervisors to observe the welding process directly — monitoring weld quality, detecting anomalies, and intervening quickly if needed. This visibility is valuable during initial production setup and for ongoing quality monitoring.
Suitable for Mobile / Flexible DeploymentOpen workstation configurations are the natural choice for mobile welding stations — systems mounted on wheeled platforms that can be repositioned between different production areas or workstations as needed. DATO's mobile cobot welding station configurations use open structures precisely because mobility and flexibility are the primary design requirements.
Limitations of Open Configuration
Laser and Arc Radiation ExposureWithout physical walls to contain laser radiation or arc flash, the surrounding workshop area requires appropriate safety controls — laser safety zones, arc flash barriers, or safety light curtains. This is manageable but requires careful safety planning and consistent operator compliance.
Welding Fume ManagementOpen workstations rely on workshop ventilation and/or portable fume extraction units to manage welding smoke and fumes. In workshops with limited ventilation or strict environmental requirements, this can be a compliance challenge.
Noise and Light Exposure to Surrounding AreasWelding arc flash and process noise are not contained by physical walls, which may be a concern in workshops where welding stations are located near other work areas or office spaces.
Less Suitable for High-Power Laser WeldingAt higher laser power levels (above 2000W), the laser safety requirements for an open configuration become more demanding. Enclosed configurations become increasingly practical as laser power increases.
Who Should Choose an Open Workstation?
Manufacturers using cobot welding systems where the robot's built-in safety features manage proximity risks
Workshops with good natural ventilation or existing fume extraction infrastructure
Production environments where part size or material handling makes enclosed operation impractical
Manufacturers who need mobile or flexible deployment across multiple production areas
Operations where fast deployment and lower initial investment are priorities
Facilities with established laser safety protocols and trained operators
Enclosed Robotic Welding Workstation
What It Is
An enclosed robotic welding workstation surrounds the robot, welding head, and workpiece within a physical protective structure — typically steel panels with safety-glass viewing windows, interlocked access doors, and integrated fume extraction. The enclosure contains laser radiation, arc flash, welding fumes, and process noise within a defined physical boundary, providing a higher level of passive safety protection for the surrounding workshop.
DATO's enclosed workstation configurations use European-standard protective covers with visible laser protective screens on the enclosure panels — providing both physical containment and optical protection against laser radiation. Welding smoke and fumes are filtered internally before exhaust, making the enclosed configuration significantly cleaner for the surrounding workshop environment.
Key Advantages of Enclosed Configuration
Comprehensive Passive Safety ProtectionThe enclosure physically contains laser radiation, arc flash, and process hazards within a defined boundary. Safety interlocks on all access doors ensure the welding process stops automatically if an operator opens the enclosure during operation. This passive safety approach reduces dependence on operator compliance with safety protocols and provides a higher baseline safety level.
This is particularly significant for high-power laser welding (1500W and above), where the laser safety requirements in an open environment are demanding. The enclosed configuration provides laser safety by containment — a fundamentally more reliable approach than relying on safety zones and operator behavior.
Integrated Fume Extraction and Air Quality ControlEnclosed workstations integrate fume extraction directly into the enclosure structure. Welding smoke and fumes are captured at the source and filtered before exhaust — keeping the surrounding workshop air clean and supporting compliance with occupational health and environmental regulations. For workshops in regions with strict air quality standards, or for manufacturers welding materials that produce hazardous fumes (galvanized steel, coated metals, certain aluminum alloys), this is a critical operational requirement.
Reduced Noise and Light Impact on Surrounding AreasThe enclosure contains welding arc flash and process noise, reducing the impact on adjacent work areas. This is valuable in workshops where welding stations are located near other production activities, quality inspection areas, or office spaces.
Cleaner Workshop EnvironmentBy containing fumes, spatter, and process byproducts within the enclosure, the surrounding workshop floor stays cleaner — reducing housekeeping requirements and improving the overall working environment.
Regulatory Compliance SupportIn many jurisdictions, enclosed welding workstations simplify compliance with laser safety regulations (IEC 60825), occupational health standards, and environmental emission requirements. The enclosure provides documented physical containment that satisfies regulatory requirements more straightforwardly than open-configuration safety management.
Professional Appearance for Customer Visits and AuditsEnclosed workstations present a professional, organized production environment that reflects well during customer factory audits, ISO certification inspections, and supplier qualification visits. This is a soft benefit, but a real one for manufacturers who regularly host customer visits.
Limitations of Enclosed Configuration
Higher Initial InvestmentThe enclosure structure, interlocked doors, safety-glass panels, integrated fume extraction, and laser protective screens add meaningful cost to the total workstation investment compared to an open configuration with equivalent robot and welding equipment.
Part Size and Loading ConstraintsThe enclosure defines a fixed maximum part size — workpieces must fit through the access doors and within the enclosure working volume. For very large parts, this is a hard constraint that may make enclosed operation impractical.
Less Flexible for RepositioningEnclosed workstations are heavier, larger, and more complex to move than open configurations. They are designed for fixed installation rather than flexible deployment.
Reduced Direct Visibility During OperationOperators observe the welding process through safety-glass viewing windows rather than directly. While this is entirely safe and functional, it provides slightly less immediate visual feedback than an open configuration.
Who Should Choose an Enclosed Workstation?
Manufacturers using high-power laser welding (1500W and above) where laser containment is the safest approach
Workshops with limited natural ventilation or strict air quality requirements
Facilities that need to meet strict laser safety, occupational health, or environmental regulations
Manufacturers who regularly host customer audits or certification inspections
Production environments where consistent, passive safety is preferred over protocol-dependent safety management
Factories where the welding workstation is located near other work areas that must be protected from arc flash, fumes, and noise

Side-by-Side Comparison: Open vs Enclosed
Factor | Open Workstation | Enclosed Workstation |
Safety approach | Active (light curtains, zones, protocols) | Passive (physical containment) |
Laser safety | Safety zones + operator protocols | Containment by enclosure |
Fume management | Workshop ventilation + portable extraction | Integrated internal extraction |
Arc flash / noise containment | Not contained | Contained within enclosure |
Part size flexibility | Unlimited — no enclosure constraint | Limited by enclosure dimensions |
Loading / unloading | Any direction, crane/forklift compatible | Through access doors |
Mobile / flexible deployment | Yes — natural fit for mobile stations | No — fixed installation |
Initial investment | Lower | Higher |
Regulatory compliance | Requires active safety management | Simpler — physical containment documented |
Workshop air quality | Depends on ventilation | Controlled — internal filtration |
Operator visibility | Direct observation | Through safety-glass windows |
Best for laser power | Up to 1500W (manageable open safety) | 1500W and above (containment preferred) |
Deployment time | Faster | Longer |
Typical applications | Mobile stations, large parts, flexible production | High-power welding, regulated environments, fixed production lines |
The Third Configuration: Mobile Welding Workstation
Beyond the open/enclosed distinction, it is worth addressing the mobile welding workstation as a distinct configuration category — because it represents a fundamentally different deployment philosophy rather than simply a variation of the open type.
A mobile robotic welding workstation mounts the robot arm, welding equipment, control system, and supporting infrastructure on a wheeled platform that can be repositioned across the production floor. The robot is typically a cobot (for safe operation in proximity to operators during transit and setup), and the overall system is designed for rapid deployment at different workstations or production areas.
When Mobile Configuration Makes Sense
Multi-Product Workshops with Shared Production AreasIf your factory produces multiple product lines in shared production areas — and different product lines need robotic welding support at different times — a mobile workstation allows a single robotic welding system to serve multiple production areas rather than requiring a dedicated fixed workstation for each.
Seasonal or Variable Production DemandManufacturers with seasonal production peaks or variable demand patterns can deploy mobile welding stations where and when they are needed, then redeploy them as production schedules change.
First Automation Step — Before Committing to Fixed InfrastructureFor manufacturers taking their first step into robotic welding automation, a mobile workstation allows production experience to be gained before committing to the fixed infrastructure of a permanent welding cell. The insights gained from operating a mobile system often inform better decisions about permanent workstation placement and configuration.
Supplementing Fixed Workstations During Peak DemandMobile workstations can supplement fixed production lines during peak demand periods — providing additional welding capacity where it is needed without permanent infrastructure investment.
Positioner Configurations: Extending Workstation Capability
One of the most important — and most frequently underspecified — aspects of robotic welding workstation design is the positioner configuration. The positioner holds and rotates the workpiece, allowing the robot to access all required weld positions without repositioning the robot itself.
Choosing the right positioner for your parts is as important as choosing the right robot and welding process. DATO workstations support the following positioner configurations:
Flat Welding Platform
The simplest configuration — a fixed flat table that holds the workpiece in a single orientation. Suitable for flat parts with welds accessible from above, or parts that can be manually repositioned between weld sequences. Used in the DATO Aubo i10 cobot workstation configurations deployed for customers in Greece and Malaysia.
Single-Axis Rotary Positioner
Rotates the workpiece around a single axis, allowing the robot to access welds on multiple faces without manual repositioning. Suitable for cylindrical parts, pipe assemblies, and components with welds on multiple sides. Used in DATO's Romanian customer configuration for pipe and structural component welding.
Dual-Axis P-Type Positioner
Provides rotation around two axes — allowing the workpiece to be tilted and rotated to present any weld position to the robot in the optimal orientation. Significantly expands the range of part geometries that can be welded without manual repositioning. Used in DATO's Swiss customer configuration for batch welding of multiple workpiece types.
Single-Axis Headstock-Tailstock Positioner
Supports long parts between two driven chucks, rotating the part along its length axis. Essential for welding long structural components, tubes, beams, and other elongated parts. Provides stable support for parts that would be difficult to fixture on a rotary table.
Selecting the Right Positioner
Part Geometry | Recommended Positioner |
Flat panels, simple brackets | Flat welding platform |
Cylindrical parts, pipe assemblies | Single-axis rotary |
Complex 3D parts, multiple weld faces | Dual-axis P-type |
Long beams, tubes, structural members | Headstock-tailstock |
Mixed part types, batch production | Dual-axis P-type (most versatile) |
Real-World Workstation Configurations: DATO Customer Examples
Understanding workstation configurations in the abstract is useful — but seeing how real manufacturers have configured their systems for specific production requirements is more instructive.
Greek Sheet Metal Fabricator — Open Cobot Workstation
Application: Welding of sheet metal components, brackets, enclosures, and structural parts.Configuration: 1500W fiber laser + Aubo i10 6-axis cobot + flat welding platform + open structure.Result: Eliminated rework and doubled welding output compared to manual welding.
The open configuration was appropriate here because the parts were standard sheet metal components with accessible weld joints, the cobot's safety features managed proximity risks, and the workshop had adequate ventilation. The flat welding platform was sufficient for the part geometry.
Romanian Manufacturer — Open Cobot Workstation with Multiple Positioners
Application: Round pipe welding and structural component welding.Configuration: 2000W laser source + Aubo i10 6-axis cobot + dual-axis positioner + single-axis positioner + flat welding platform.Result: Automated pipe and structural welding with consistent quality across multiple part types.
The multi-positioner configuration allowed a single workstation to handle both cylindrical pipe parts (single-axis rotary) and flat structural components (welding platform) — maximizing the utilization of a single robotic system across different production requirements.
Swiss Manufacturer — Open Cobot Workstation, Batch Multi-Part Production
Application: Batch welding of multiple different workpiece types.Configuration: 2000W laser source + cobot + dual-axis P-type positioner.Result: Streamlined batch welding across multiple workpiece types with minimal changeover time.
The dual-axis positioner's flexibility to handle different part geometries made it the right choice for a manufacturer with a varied production schedule. The open configuration allowed quick fixture changes between part types.
Filipino Manufacturer — Industrial Robot Workstation
Application: Stainless steel pipe welding.Configuration: LA1813-25 industrial 6-axis robot.Result: Eliminated weld defects and tripled output compared to manual welding.
The industrial robot configuration was appropriate for the high-volume, fixed-production pipe welding application — where maximum throughput and repeatability on a single part type justified the higher integration investment.
U.S. Playground Equipment Manufacturer — Mobile MIG Cobot Workstation
Application: Structural tube and frame welding for playground equipment.Configuration: MIG cobot welding station, mobile open configuration.Result: Resolved welding bottleneck and improved weld consistency for structural components.
The mobile configuration was the right choice for this manufacturer because the production layout required welding support at multiple locations on the production floor, and the varied part geometry of playground equipment benefited from the cobot's flexible programming.
How to Choose Your Workstation Configuration: A Practical Framework
Work through these five questions to identify the right workstation configuration for your production:
Step 1: What is your welding process and power level?
Laser welding at 1500W or above → Enclosed configuration strongly recommended
Laser welding at 1000W–1500W, or TIG/MIG welding → Open or enclosed both viable; assess other factors
Step 2: What are your workshop ventilation and air quality requirements?
Limited ventilation, strict air quality standards, or hazardous fume materials → Enclosed with integrated extraction required
Good ventilation, standard materials → Open with portable extraction viable
Step 3: What is the size and geometry of your largest regular production part?
Parts too large to fit through an enclosure door → Open configuration required
Standard fabrication parts (within 1,500mm) → Both configurations viable
Step 4: Do you need mobile or fixed deployment?
Mobile — multiple production areas or flexible deployment → Open mobile configuration
Fixed production line → Either open or enclosed fixed installation
Step 5: What are your regulatory and customer audit requirements?
Strict laser safety regulations, ISO certification, or regular customer audits → Enclosed configuration preferred
Standard workshop safety requirements → Open configuration viable with proper safety management
DATO's Robotic Welding Workstation Solutions
DATO configures robotic welding workstations across the full range of types and applications — from compact open cobot stations for first-time automation buyers to fully enclosed high-power industrial robot cells for heavy-duty production environments.
Standard Workstation Configurations Available:
Open cobot laser welding workstation — Aubo i10 6-axis cobot + automatic laser welding head + flat welding platform + safety light curtain. Available with 1000W–3000W fiber laser source. Suitable for sheet metal fabrication, kitchen equipment, enclosures, and general metal fabrication.
Open cobot workstation with positioner — Aubo i10 6-axis cobot + laser welding head + single-axis rotary, dual-axis P-type, or headstock-tailstock positioner. Suitable for pipe welding, structural components, and multi-face welding applications.
Mobile cobot welding station — Cobot welding system on wheeled platform for flexible deployment. Available with laser, TIG, or MIG welding process.
Enclosed laser welding workstation — Full European-standard protective enclosure + laser protective screen + integrated fume extraction + interlocked access doors. Available with cobot or industrial robot, 1000W–3000W laser power.
Industrial robot welding workstation — LA1813-25 or equivalent industrial 6-axis robot + automatic welding head + positioner configuration. For high-volume, fixed-production applications.
Every DATO workstation configuration is customized to the customer's specific material, part geometry, production volume, workshop layout, and safety requirements. There is no standard "off-the-shelf" workstation — because the right workstation is the one that fits your production, not a generic template.
Related reading:
Industrial Robot Laser Welding vs Collaborative Robot Welding: Which Is Right for Your Factory?
Robotic TIG Welding vs Robotic Laser Welding: Which Process Is Right for Your Application?
Robotic Laser Welding Machine: The Complete Buyer's Guide for Manufacturers (2026)

Frequently Asked Questions
Q1: What is the difference between a robotic welding workstation and a robotic welding cell?
The terms are often used interchangeably. In practice, "welding cell" tends to refer to larger, more complex systems — often with multiple robots, automated material handling, and full production line integration — while "welding workstation" typically refers to a single-robot system designed for a specific production task. DATO's configurations are workstations in this sense: single-robot systems configured for a specific application, which can be integrated into larger production lines if required.
Q2: Can I add an enclosure to an open workstation later?
Yes, in principle — but it is more cost-effective to specify the enclosure at the time of initial purchase if you anticipate needing it. Retrofitting an enclosure requires modifications to the workstation layout, safety interlock integration, and fume extraction routing that are more complex and expensive than specifying them from the start.
Q3: How long does it take to deploy a robotic welding workstation?
Deployment time depends on configuration complexity, fixture design, and programming requirements. Open cobot workstations with standard positioner configurations can typically be deployed and producing parts within 1–3 weeks. Enclosed workstations and industrial robot configurations with complex fixtures may require 4–8 weeks for full deployment and production commissioning.
Q4: Do I need a specialist integrator to set up a DATO robotic welding workstation?
DATO provides installation guidance, operation manuals, training videos, and remote technical support. For cobot workstation configurations, the programming interface is designed to be operator-manageable without specialist robot programming expertise. For more complex industrial robot configurations, DATO's engineering team provides more intensive setup support.
Q5: What positioner configuration is most versatile for mixed production?
The dual-axis P-type positioner is the most versatile choice for manufacturers with varied part types. Its ability to tilt and rotate the workpiece to any orientation allows it to handle a wider range of part geometries than a single-axis rotary positioner, while remaining more compact than a headstock-tailstock configuration. DATO's Swiss and Romanian customer deployments both demonstrate the dual-axis positioner's effectiveness for multi-part batch production.
Q6: Can the same workstation be used for both laser welding and TIG welding?
The robot arm and workstation structure are process-agnostic — the same physical workstation frame, positioner, and safety infrastructure can support different welding processes. However, the welding head, power source, and some process-specific components are different for laser and TIG welding. Switching between processes requires changing the welding equipment, not the entire workstation.
Q7: Can DATO provide a workstation configured for my specific parts before I commit to a purchase?
Yes. DATO offers free welding sample testing and process consultation. Provide your material type, thickness, part geometry, joint design, and production volume — and DATO's engineering team will recommend the appropriate workstation configuration and produce sample welds to validate the process before purchase. Contact DATO here to arrange your consultation.
Ready to configure the right robotic welding workstation for your factory?
Explore the DATO DT-HJR Robotic Laser Welding Machine Request a Free Workstation Configuration Consultation Get a Free Welding Sample Test on Your Parts View All DATO Laser Welding Solutions
Shandong Dato Machinery Co., Ltd. — Laser Industry Leader Since 2007 info@datolaser.com | WhatsApp: +86-199-0541-0296 | www.datolaser.com
Related Blogs
-
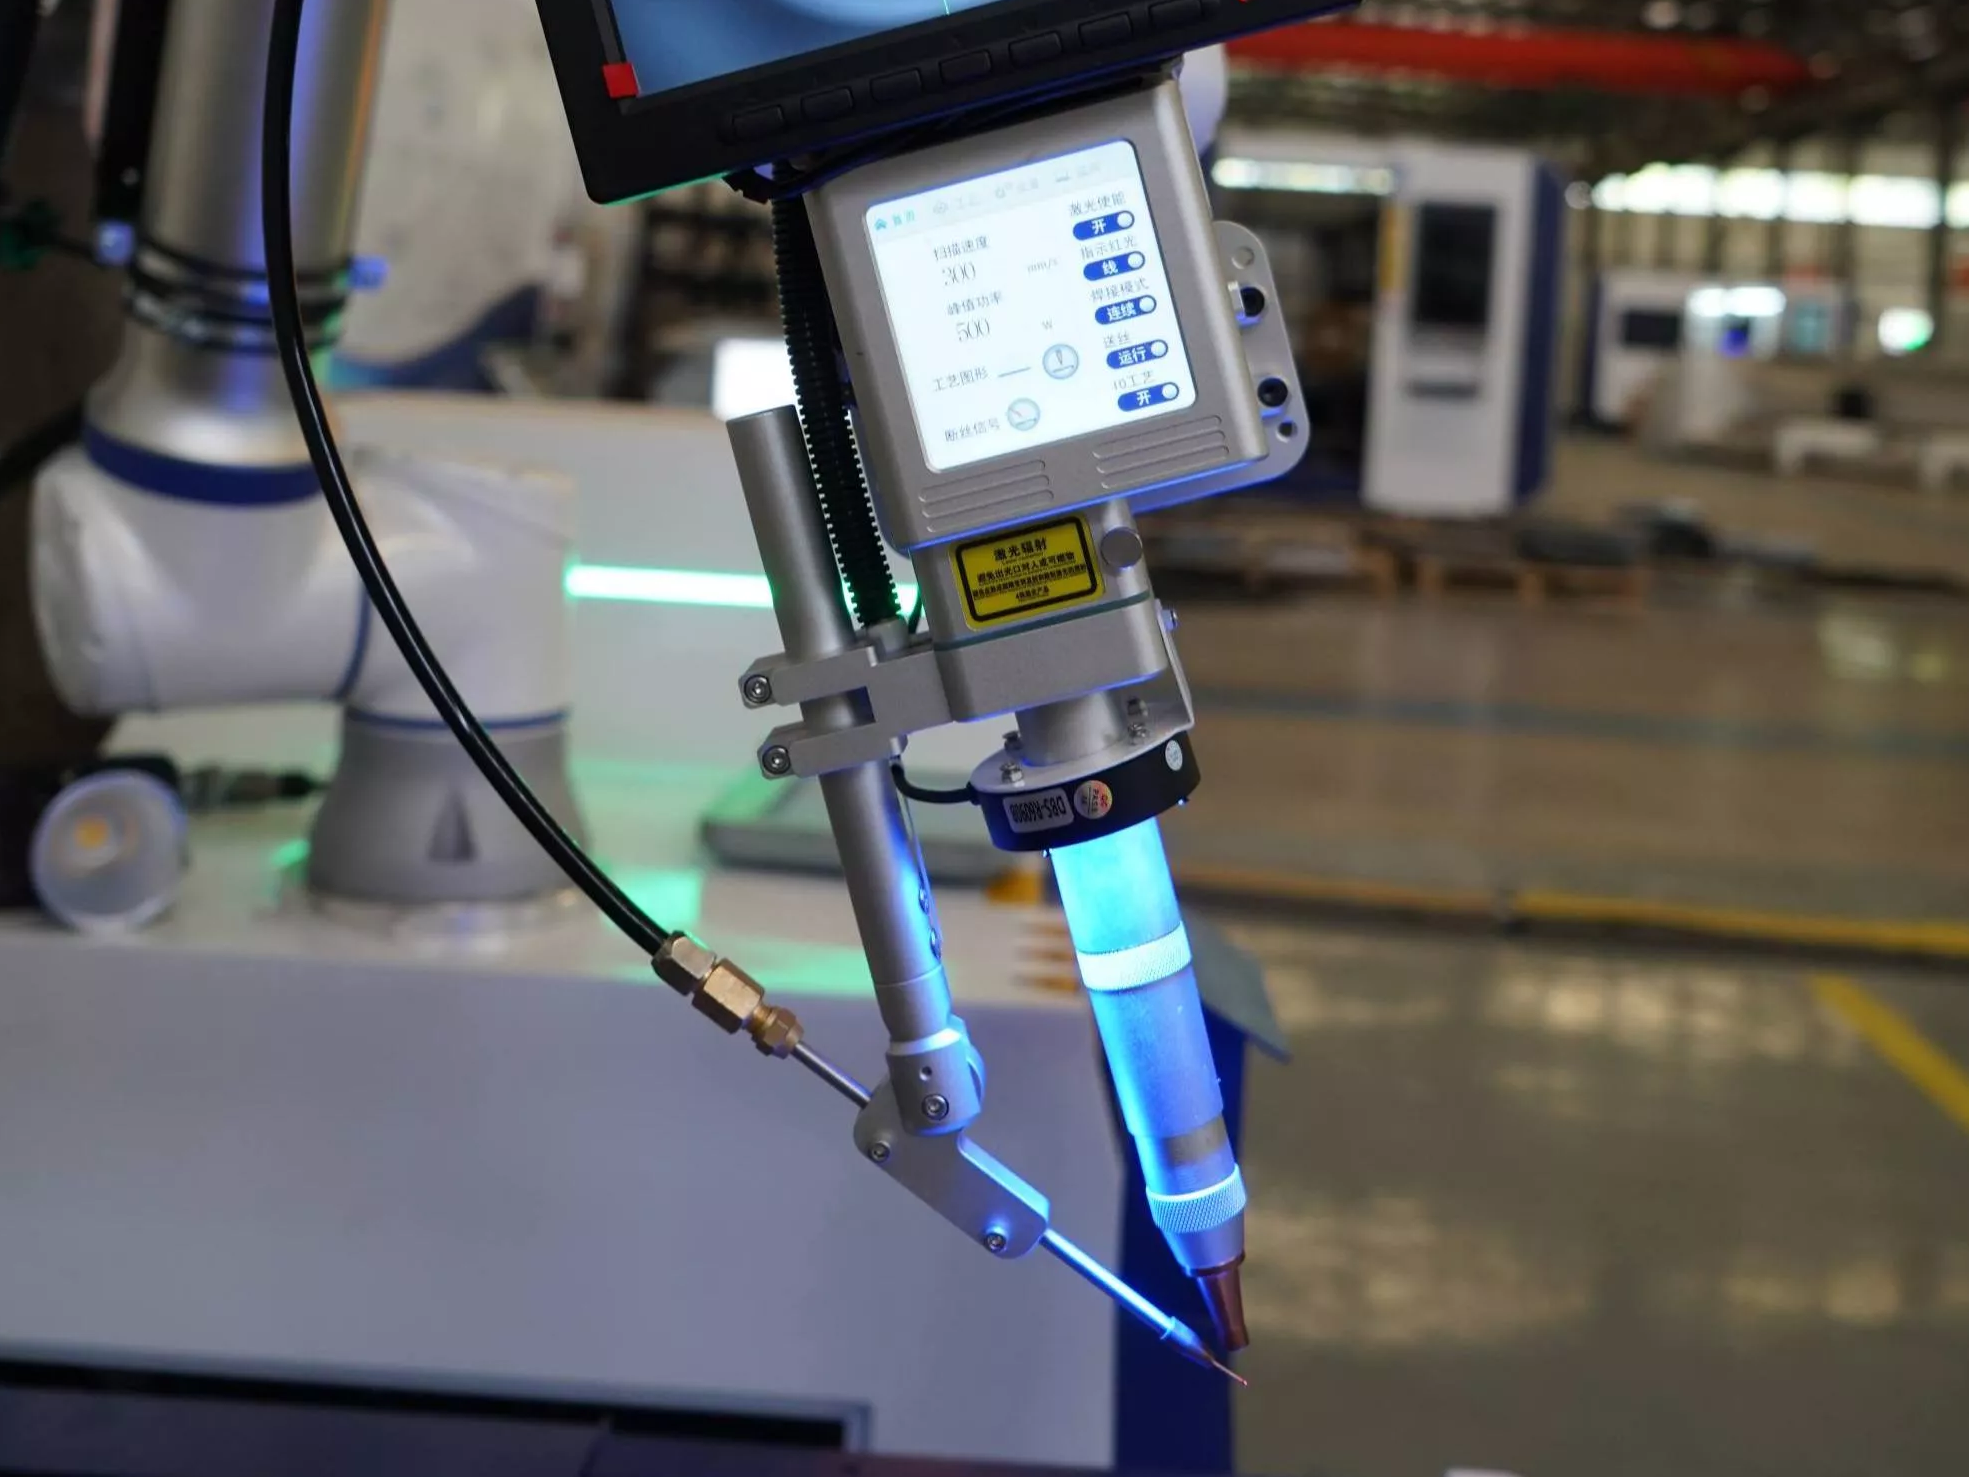 Why Manufacturers Are Buying Laser Welding Robots During The DATO LASER September Sourcing Sale 2026In 2026, manufacturers across the world are accelerating investments in laser welding robots, robotic laser welding systems, and other forms of smart manufacturing equipment to improve welding precision, reduce labor dependency, and build more efficient production lines.During the September SourcingBuyer's Guide
-
 DATO LASER Launches September Sourcing Sale with Up to 15% DiscountDATO LASER is proud to announce its September Sourcing Sale, running throughout the New Trade Festival period. This limited-time promotion offers customers up to 15% off on selected laser welding systems and CNC press brakes, along wBuyer's Guide
-
 Choosing a robotic welding system is not simply a choice between one robot brand and another. The right solution depends on your part size, weight, weld type, batch volume, changeover frequency, available floor space and required automation level.For many small and medium-sized metal fabrication shoBuyer's Guide
-
 Welding Positioner Types for Robotic Laser Welding: How to Choose the Right One for Your PartsMost buyers spend considerable time selecting the right robot arm and laser source for their robotic welding workstation. Far fewer give the same attention to the positioner — the component that holds, orieBuyer's Guide
