


Both robotic TIG welding and robotic laser welding produce high-quality, clean welds on stainless steel and aluminum. Both can be fully automated. Both are used by precision manufacturers worldwide. So why does choosing between them matter — and how do you make the right call for your specific application?
The answer lies in the details: material thickness, joint design, production volume, weld appearance requirements, operating cost, and the specific quality standards your customers demand. Choose the wrong process, and you either overspend on capability you don't need, or find yourself unable to meet the quality or throughput requirements your production demands.
This guide gives you a complete, technically grounded comparison of robotic TIG (argon arc) welding and robotic laser welding — covering the physics of each process, their practical performance differences, cost structures, and the specific scenarios where each genuinely excels.

Understanding the Two Processes
Robotic TIG Welding (GTAW / Argon Arc Welding)
TIG welding — formally known as Gas Tungsten Arc Welding (GTAW), and widely referred to as argon arc welding in manufacturing — uses a non-consumable tungsten electrode to generate an electric arc that melts the base metal. Argon gas (or argon-helium mixtures) shields the weld pool from atmospheric contamination. Filler wire can be added manually or automatically via a wire feeder.
When integrated with a robotic arm, TIG welding becomes a highly repeatable, programmable process capable of producing exceptionally clean, precise weld seams — particularly on stainless steel, aluminum, titanium, and other materials where weld purity and appearance are critical.
DATO's robotic TIG welding stations — available in both open and enclosed configurations — combine a robotic arm with a professional TIG welding power source, argon gas delivery system, wire feeding unit, and control system. The enclosed configuration adds full protective housing with integrated fume extraction, making it suitable for workshops with strict safety and environmental requirements.
Robotic Laser Welding
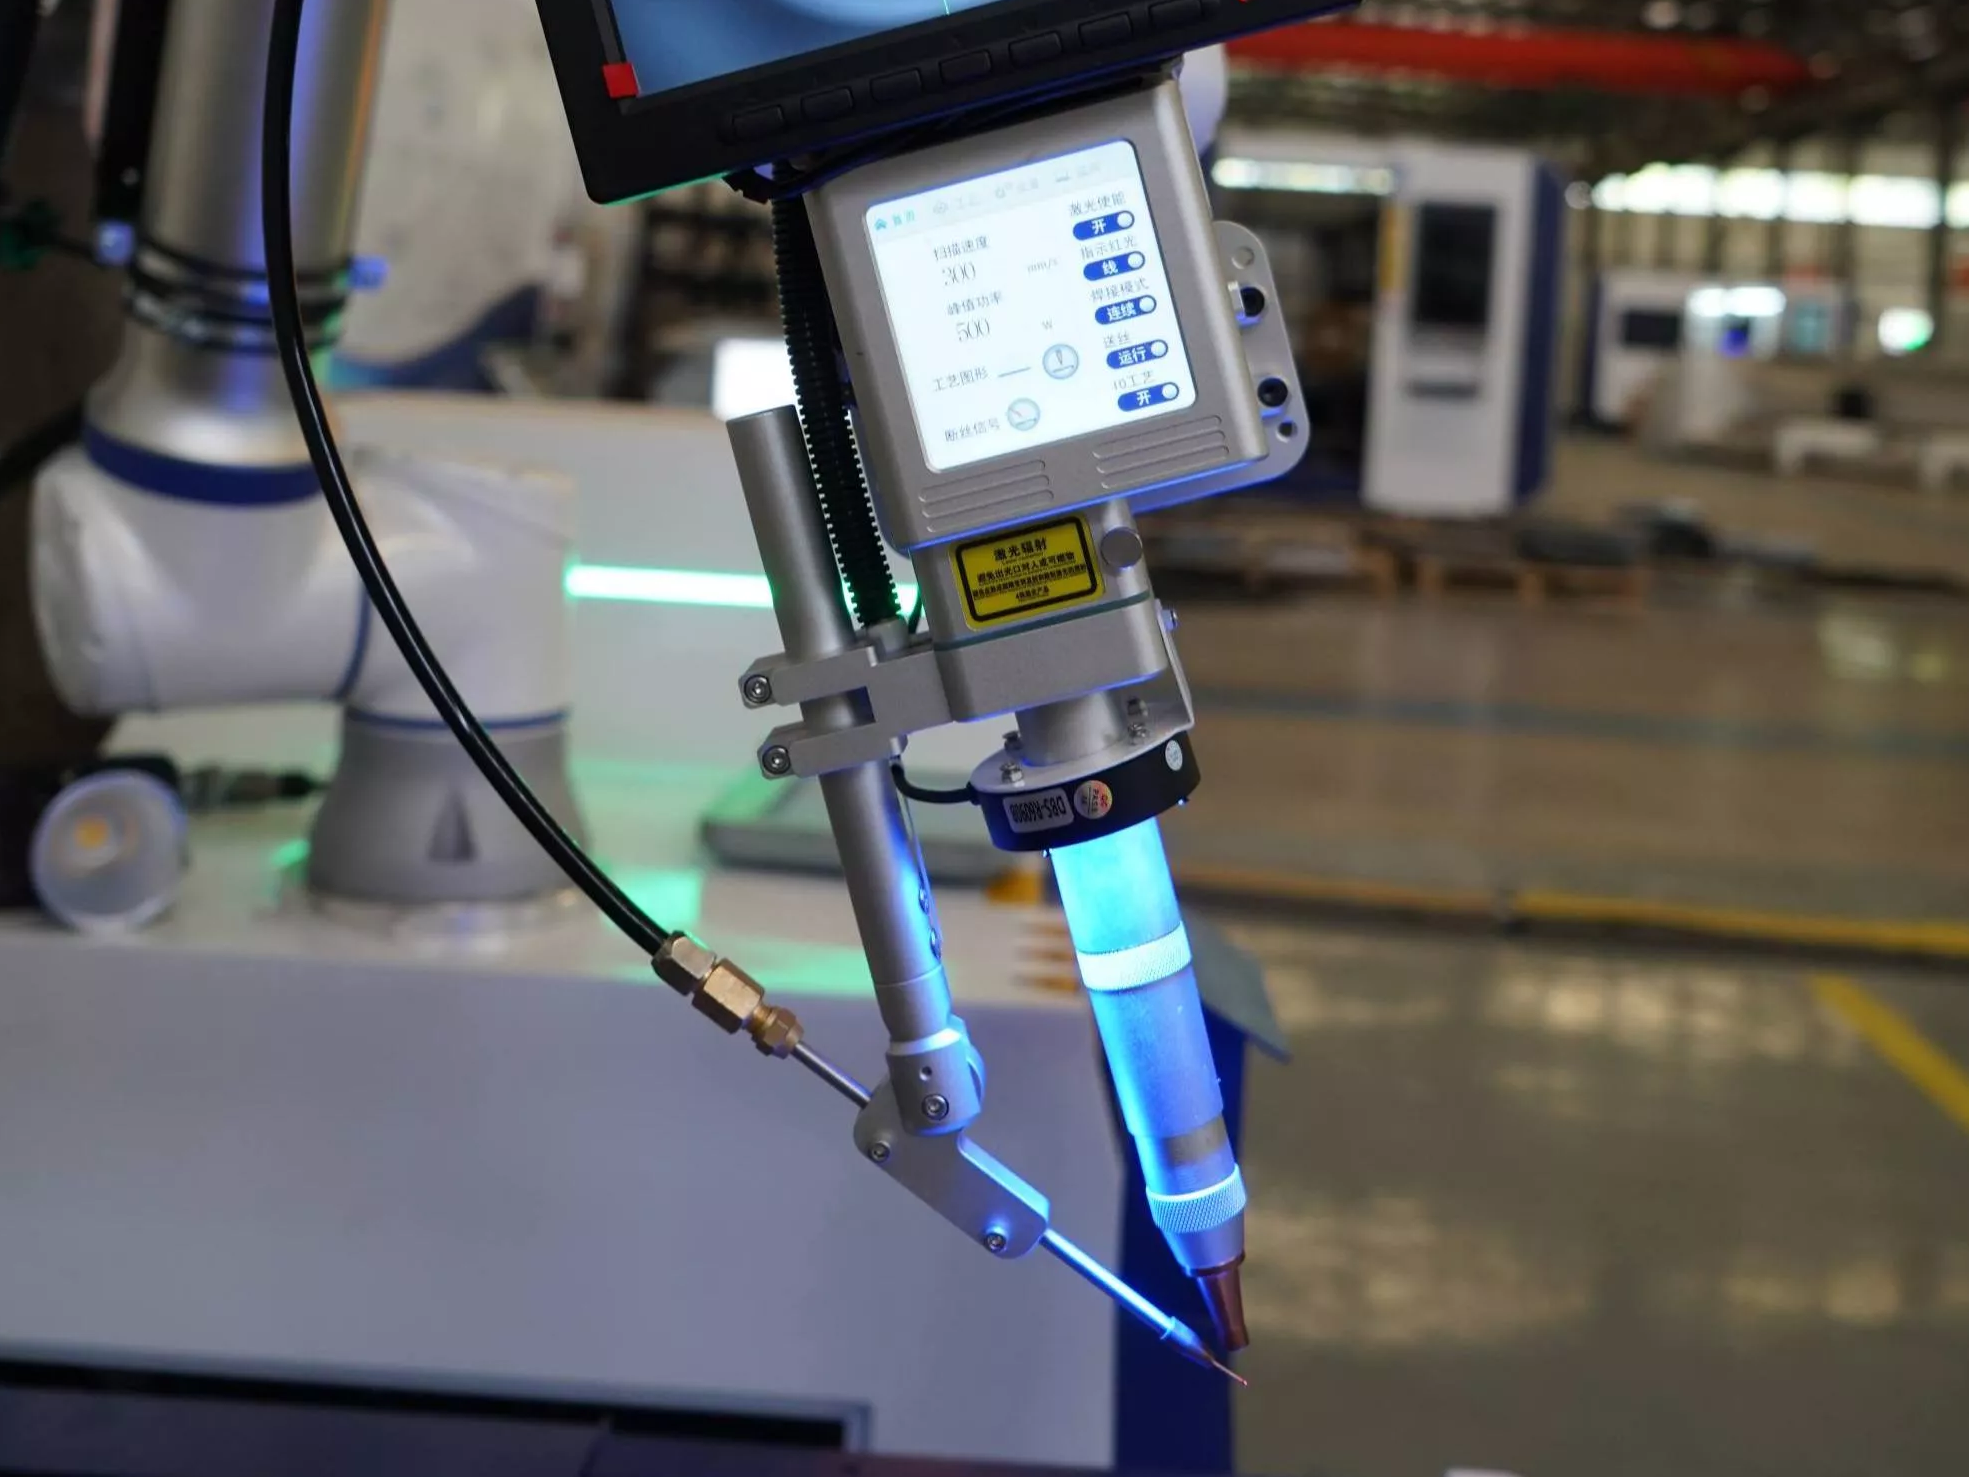
Robotic laser welding uses a focused high-power fiber laser beam — delivered through an automatic welding head mounted on a robotic arm — to melt and fuse metal with extreme precision. The laser's concentrated energy density produces a narrow, deep weld with a very small heat-affected zone.
The DATO DT-HJR Robotic Laser Welding Machine combines a 6-axis collaborative robot with a fiber laser source (1000W–3000W), automatic laser welding head, and wire feeding system. It is designed for manufacturers who need fast, clean, automated welding of stainless steel, carbon steel, aluminum alloy, and galvanized sheet in batch production environments.
The Physics Behind the Difference
To understand why these two processes perform differently, it helps to understand the fundamental physics of how each delivers energy to the weld zone.
TIG welding generates heat through an electric arc — a relatively broad, diffuse energy source. The arc heats a larger area of the base metal, producing a wider weld pool with more heat input per unit length of weld. This broader heat distribution is actually an advantage in certain applications: it allows the weld pool to flow and wet out across wider gaps, and it gives the welder (or robot) more tolerance for joint fit-up variation.
Laser welding delivers energy through a focused laser beam — an extremely concentrated, high-intensity energy source. The laser creates a narrow "keyhole" in the metal, with energy density orders of magnitude higher than a TIG arc. This produces a deep, narrow weld with a very small heat-affected zone and minimal thermal distortion. The trade-off is that the process is less tolerant of joint fit-up gaps — the laser beam requires tight, consistent joint contact to weld effectively.
This single physical difference — broad diffuse arc vs. concentrated laser beam — explains most of the practical performance differences between the two processes.

Comprehensive Process Comparison
Weld Quality and Appearance
Dimension | Robotic TIG Welding | Robotic Laser Welding |
Weld seam width | Wider (2–6mm typical) | Narrower (0.3–2mm typical) |
Weld depth-to-width ratio | Lower (broader, shallower profile) | Higher (deep, narrow profile) |
Surface appearance | Smooth, bright, excellent aesthetics | Very smooth, minimal oxidation, excellent aesthetics |
Post-weld grinding required | Minimal to none for skilled setup | Minimal to none |
Weld porosity | Low with proper shielding | Very low |
Undercut risk | Low with correct parameters | Low with correct parameters |
Spatter | None (TIG is spatter-free) | None (laser welding is spatter-free) |
Weld color (stainless steel) | Silver to light gold with argon shielding | Silver, minimal discoloration |
Assessment: Both processes produce excellent weld appearance. For the narrowest, most precise weld seams on thin material, laser welding has a structural advantage due to its concentrated energy. For applications where a slightly wider, more filled weld profile is preferred — or where the weld must bridge a small gap — TIG welding's broader heat input is advantageous.
Heat Input and Thermal Distortion
This is one of the most practically significant differences between the two processes — and the one that most directly affects part quality for precision applications.
Dimension | Robotic TIG Welding | Robotic Laser Welding |
Heat input per unit length | Moderate to high | Very low |
Heat-affected zone (HAZ) width | Wider | Narrow |
Thermal distortion on thin sheet | Moderate — requires careful parameter control | Very low — minimal distortion even on thin material |
Warping risk on 0.5–2mm sheet | Present — requires fixturing and sequencing | Very low |
Residual stress in weld zone | Moderate | Low |
Metallurgical changes in HAZ | More extensive | Minimal |
Assessment: For thin sheet metal (0.5–3mm), laser welding's low heat input is a decisive advantage. The minimal thermal distortion means less fixturing complexity, less post-weld straightening, and better dimensional accuracy on finished parts. For thicker materials (above 4–6mm) where distortion is less of a concern, the heat input difference becomes less significant.
Material Thickness Range
Material | TIG Welding Range | Laser Welding Range | Notes |
Stainless steel | 0.5mm–unlimited | 0.3mm–8mm (standard power) | Laser excels thin; TIG better for thick |
Carbon steel | 0.5mm–unlimited | 0.5mm–8mm (standard power) | TIG less common for carbon steel |
Aluminum alloy | 0.8mm–unlimited | 0.5mm–6mm (standard power) | Both viable; TIG uses AC for aluminum |
Titanium | 0.3mm–unlimited | 0.3mm–4mm | TIG dominant for titanium |
Copper / brass | Possible (challenging) | 0.5mm–4mm | Laser generally preferred for copper |
Galvanized sheet | Not recommended | 0.5mm–4mm | Laser handles galvanized well |
Dissimilar metals | Limited | Possible for some combinations | Laser more flexible |
Assessment: TIG welding has a broader thickness range — particularly for thick material — because the arc process scales to any thickness with appropriate multi-pass techniques. Laser welding at standard power levels (1000W–3000W) is optimized for thin to medium sheet. For material above 6–8mm, TIG welding or high-power laser welding becomes necessary.
Welding Speed and Production Throughput
Scenario | Robotic TIG Welding | Robotic Laser Welding |
Thin sheet (1mm stainless steel) | Moderate speed | Fast — 2–5× faster than TIG |
Medium sheet (3mm stainless steel) | Moderate speed | Fast — 1.5–3× faster than TIG |
Thick plate (8mm+ stainless steel) | Multi-pass — slower overall | Not applicable at standard power |
Long straight seams | Consistent speed | Very fast |
Complex curved paths | Good — arc follows path well | Good — laser head follows path well |
Cycle time for batch production | Longer | Shorter |
Assessment: For thin to medium sheet metal in batch production, robotic laser welding is significantly faster than robotic TIG welding. This speed advantage directly translates to higher throughput and lower cost per part. For thick material requiring multi-pass welding, TIG welding is the practical choice.
Joint Fit-Up Tolerance
This is a critical practical consideration that is often underestimated in process selection.
Dimension | Robotic TIG Welding | Robotic Laser Welding |
Maximum gap tolerance | Up to 1–2mm with filler wire | Typically ≤0.3–0.5mm |
Joint preparation requirement | Moderate — standard machined or cut edges | Higher — tight fit-up required |
Part consistency requirement | Moderate | Higher |
Fixture precision requirement | Moderate | Higher |
Sensitivity to part variation | Lower | Higher |
Assessment: This is TIG welding's most significant practical advantage over laser welding. The broader arc can bridge gaps that would cause laser welding to fail or produce defective welds. For manufacturers whose parts have variable fit-up quality — due to cutting tolerances, forming variation, or part design — TIG welding is more forgiving. For manufacturers with tight part consistency and precision fixtures, laser welding's gap sensitivity is manageable.
Operating Cost Analysis
Cost Component | Robotic TIG Welding | Robotic Laser Welding |
Consumables — electrode | Tungsten electrode (long life, low cost) | None |
Consumables — filler wire | Required for most applications | Optional (autogenous welding possible) |
Shielding gas | Argon — continuous consumption | Argon or nitrogen — lower consumption |
Energy consumption | Moderate | Moderate to high (laser source) |
Maintenance complexity | Low — robust, proven technology | Moderate — laser source and optics |
Spare parts cost | Low | Moderate (protective lens, nozzle) |
Post-weld processing | Minimal | Minimal |
Overall operating cost | Lower | Moderate |
Assessment: Robotic TIG welding has lower consumable and maintenance costs. However, laser welding's higher speed means fewer machine-hours per part — which reduces labor and overhead cost per unit. At high production volumes, laser welding's speed advantage often offsets its higher equipment and maintenance cost, resulting in a lower total cost per part.
Equipment Investment
Component | Robotic TIG Welding Station | Robotic Laser Welding System |
Robot arm | Similar | Similar |
Welding power source / laser source | Lower (TIG power source) | Higher (fiber laser source) |
Welding head / torch | Lower cost | Higher cost (automatic welding head) |
Wire feeding system | Standard | Standard |
Shielding gas system | Standard argon supply | Standard argon/nitrogen supply |
Safety enclosure | Optional | Recommended (laser safety) |
Total system investment | Lower | Higher |
Assessment: Robotic TIG welding stations have a lower initial investment than robotic laser welding systems of equivalent robot specification. For manufacturers where budget is the primary constraint and production speed is not critical, TIG welding offers a more accessible entry point to robotic welding automation.

Full Comparison Summary Table
Factor | Robotic TIG Welding | Robotic Laser Welding | Winner |
Weld appearance | Excellent | Excellent | Draw |
Weld seam width | Wider | Narrower | Laser (precision) |
Heat input | Moderate–high | Very low | Laser |
Distortion on thin sheet | Moderate | Very low | Laser |
Welding speed | Moderate | Fast | Laser |
Thickness range | 0.5mm–unlimited | 0.3–8mm (std power) | TIG (thick material) |
Gap / fit-up tolerance | High (up to 2mm) | Low (≤0.5mm) | TIG |
Material versatility | Very broad | Broad | TIG |
Consumable cost | Low | Moderate | TIG |
Equipment investment | Lower | Higher | TIG |
Batch production throughput | Moderate | High | Laser |
Automation suitability | Excellent | Excellent | Draw |
Fixture precision required | Moderate | High | TIG |
When to Choose Robotic TIG Welding
Robotic TIG welding is the right choice when one or more of the following conditions apply to your production:
1. Your Parts Have Variable Fit-Up Quality
If your parts are cut, formed, or fabricated with tolerances that result in joint gaps above 0.5mm, TIG welding's gap-bridging capability is essential. Trying to laser weld parts with inconsistent fit-up will result in defects, rework, and frustration.
2. You Weld Thick Material (Above 6–8mm)
For stainless steel or aluminum above 6–8mm thickness, standard-power robotic laser welding reaches its practical limit. TIG welding scales to any thickness through multi-pass techniques and is the established process for thick precision metal fabrication.
3. You Work with Titanium or Specialty Alloys
TIG welding is the dominant process for titanium, Inconel, and other specialty alloys used in aerospace, medical, and chemical processing applications. The process's precise heat control and excellent shielding gas coverage make it the preferred choice for these materials.
4. Budget Is the Primary Constraint
If initial investment is the primary decision factor and production speed is not critical, robotic TIG welding stations offer a lower entry cost to robotic welding automation.
5. Your Welds Must Meet Specific Weld Profile Standards
Some welding standards and customer specifications require a specific weld bead profile — width, reinforcement height, toe angle — that is more naturally achieved with TIG welding's broader heat input and filler wire control.
When to Choose Robotic Laser Welding
Robotic laser welding is the right choice when one or more of the following conditions apply:
1. You Weld Thin Sheet Metal (0.3–4mm) at Production Volume
Laser welding's combination of low heat input (minimal distortion) and high speed makes it the optimal process for thin sheet metal in batch production. For stainless steel kitchen equipment, electrical cabinets, sheet metal enclosures, and similar applications, robotic laser welding delivers better quality and higher throughput than TIG welding.
2. Thermal Distortion Is a Critical Quality Concern
For precision parts where dimensional accuracy after welding is critical — thin-wall components, assemblies with tight tolerances, visible exterior surfaces — laser welding's minimal heat input is a decisive advantage. Less distortion means less fixturing complexity, less post-weld straightening, and better first-pass yield.
3. Production Speed and Throughput Are Competitive Priorities
If your business competes on delivery speed, or if cutting cycle time is essential to your production economics, laser welding's speed advantage on thin to medium material is directly relevant to your bottom line.
4. You Weld Galvanized Sheet, Copper, or Brass
Laser welding handles galvanized steel, copper, and brass more effectively than TIG welding in most production scenarios. The laser's precise energy control manages the reflectivity and thermal conductivity challenges of these materials better than a TIG arc.
5. You Need Clean Welds with Minimal Post-Processing
Laser welding produces clean, narrow weld seams with minimal spatter, oxidation, or discoloration — reducing or eliminating post-weld grinding, polishing, and cleaning operations. For manufacturers where post-weld processing is a significant time and cost factor, this is a meaningful operational advantage.
Application Matching: Industry by Industry
Stainless Steel Kitchen and Bathroom Equipment
Typical material: 1–3mm stainless steel. Joint types: butt, fillet, corner. Quality requirement: clean appearance, no discoloration.
Recommendation: Robotic Laser Welding
The thin material, high appearance requirement, and batch production volume all favor laser welding. The DATO DT-HJR at 1500W–2000W is the standard configuration for this application. Low heat input means minimal distortion on thin stainless steel panels, and the clean weld seam typically requires no post-weld polishing.
Precision Stainless Steel Food Processing Equipment
Typical material: 2–6mm stainless steel 316L. Joint types: butt, fillet. Quality requirement: full penetration, smooth internal surface, hygienic weld profile, possible weld inspection.
Recommendation: Robotic TIG Welding (open or enclosed station)
Food processing equipment often requires full-penetration welds with smooth internal surfaces that meet hygienic design standards. TIG welding's precise heat control, excellent shielding, and ability to produce consistent full-penetration welds on 2–6mm material make it the preferred process. The enclosed TIG welding station configuration provides the clean, controlled environment appropriate for this quality level.
Aluminum Alloy Structural Components
Typical material: 2–6mm aluminum alloy (5052, 6061). Joint types: butt, fillet, T-joint. Quality requirement: structural integrity, acceptable appearance.
Recommendation: Robotic TIG Welding
Aluminum TIG welding uses alternating current (AC) to provide the oxide-cleaning action essential for quality aluminum welds. For structural aluminum components where weld integrity is the primary requirement and material thickness is above 3mm, robotic TIG welding is the established process. For thin aluminum sheet (below 2mm) where distortion is a concern, laser welding becomes competitive.
Sheet Metal Enclosures and Electrical Cabinets
Typical material: 1–3mm carbon steel and stainless steel. Joint types: corner, fillet, lap. Quality requirement: consistent appearance, no burn-through, batch production.
Recommendation: Robotic Laser Welding
The combination of thin material, batch production, and appearance requirements strongly favors laser welding. The DATO DT-HJR handles this application with excellent consistency and speed.
Aerospace and Medical Device Components
Typical material: Titanium, stainless steel 316L, Inconel, 0.3–4mm. Joint types: butt, edge. Quality requirement: highest purity, full penetration, X-ray or dye-penetrant inspection.
Recommendation: Robotic TIG Welding (enclosed station)
Aerospace and medical welding standards typically specify TIG welding for titanium and high-alloy materials. The enclosed station configuration with inert gas purging provides the contamination-free environment required for these applications. Laser welding can be used for some aerospace applications, but TIG welding remains the dominant process for the highest-specification work.
Advertising Signs and Decorative Metal Products
Typical material: 0.5–2mm stainless steel, aluminum, brass. Joint types: butt, corner, edge. Quality requirement: excellent surface appearance, no grinding marks.
Recommendation: Robotic Laser Welding
The thin material and high appearance requirement favor laser welding. The narrow, clean weld seam with minimal heat discoloration is ideal for visible decorative applications.
The Hybrid Approach: When to Use Both
Some manufacturers operate both robotic TIG and robotic laser welding in the same facility — using each process for the applications it handles best:
Laser welding for thin sheet metal production lines where speed and low distortion are priorities
TIG welding for thicker material, specialty alloys, or applications requiring gap-bridging capability
This hybrid approach is increasingly common in precision metal fabrication facilities and represents a mature process strategy that maximizes the strengths of both technologies.
DATO's Robotic Welding Solutions
DATO offers robotic welding automation across both process types:
Robotic Laser Welding:The DT-HJR Robotic Laser Welding Machine — 6-axis collaborative robot, automatic laser welding head, 1000W–3000W fiber laser source, wire feeding system. Suitable for stainless steel, carbon steel, aluminum alloy, galvanized sheet, and other metals. Available with optional safety enclosure, smoke purifier, gun cleaning system, and wire cutting system.
Robotic TIG (Argon Arc) Welding Stations:DATO robotic TIG welding stations are available in open and enclosed configurations, combining a robotic arm with a professional TIG welding power source, argon gas delivery, wire feeding unit, and control system. The enclosed configuration adds full protective housing with integrated fume extraction — suitable for workshops requiring strict safety, environmental, and quality control standards.
Not sure which process fits your application? DATO's engineering team provides free process consultation and welding sample testing on customer-supplied materials. Share your material type, thickness, joint design, quality requirements, and production volume — and we will recommend the right welding process and system configuration for your specific needs.
Related reading:
Industrial Robot Laser Welding vs Collaborative Robot Welding: Which Is Right for Your Factory?
How a Robotic Laser Welding Machine Pays for Itself — ROI, Productivity & Real Cost Analysis
Robotic Laser Welding Machine: The Complete Buyer's Guide for Manufacturers (2026)
Summary: The One-Page Decision Guide
Your Situation | Choose Robotic TIG Welding | Choose Robotic Laser Welding |
Material thickness | Above 6mm, or multi-pass required | 0.3–6mm thin to medium sheet |
Joint fit-up quality | Variable, gaps up to 2mm | Consistent, tight fit-up (≤0.5mm) |
Primary material | Titanium, specialty alloys, thick SS/Al | Stainless steel, carbon steel, galvanized, copper |
Distortion sensitivity | Moderate | High — thin sheet, precision parts |
Production speed priority | Moderate | High — batch production throughput |
Budget | Lower initial investment preferred | Higher investment, lower cost per part at volume |
Industry | Food processing, aerospace, medical, heavy fabrication | Kitchen equipment, sheet metal, enclosures, advertising |
Post-weld processing | Acceptable | Minimize grinding and polishing |
DATO solution | Robotic TIG Welding Station (open or enclosed) |

Frequently Asked Questions
Q1: Is TIG welding better than laser welding for stainless steel?
It depends on the application. For thin stainless steel (0.5–4mm) in batch production where speed and low distortion are priorities, robotic laser welding typically delivers better results. For thicker stainless steel (above 6mm), full-penetration food-grade welds, or applications requiring gap-bridging capability, robotic TIG welding is often the better choice. Many manufacturers use both processes for different product lines.
Q2: Can laser welding replace TIG welding completely?
For many thin sheet metal applications — kitchen equipment, enclosures, sheet metal fabrication — laser welding has largely replaced TIG welding in modern production facilities. However, for thick material, titanium, specialty alloys, and applications requiring gap-bridging capability, TIG welding remains the preferred or required process. A complete replacement is not realistic for all applications.
Q3: Which process produces a cleaner weld appearance?
Both processes produce excellent weld appearance when properly set up. Laser welding produces a narrower weld seam with less heat discoloration, which is preferred for visible decorative applications. TIG welding produces a slightly wider, more filled weld profile that is preferred for some structural and food-grade applications.
Q4: What is the argon gas consumption difference between TIG and laser welding?
TIG welding requires continuous argon shielding of both the weld pool and the tungsten electrode — typically 8–15 L/min during welding. Laser welding uses argon or nitrogen as a shielding gas at lower flow rates (typically 5–10 L/min), and only during the actual welding pass. For high-volume production, laser welding's lower gas consumption is a meaningful operating cost advantage.
Q5: Can DATO's robotic TIG welding station weld aluminum?
Yes. DATO's robotic TIG welding stations support aluminum welding using AC (alternating current) TIG welding, which provides the oxide-cleaning action essential for quality aluminum welds. The specific configuration — AC/DC TIG power source, tungsten electrode type, shielding gas mixture — is selected based on the aluminum alloy and thickness.
Q6: What is the difference between DATO's open and enclosed TIG welding station configurations?
The open configuration provides easier access for loading and unloading large or irregular parts, and is suitable for workshops with good ventilation and standard safety requirements. The enclosed configuration adds full protective housing with integrated fume extraction and safety interlocks — providing better operator protection, cleaner working environment, and compliance with stricter safety and environmental standards. Both configurations are available with the same robot and welding power source options.
Q7: Can DATO provide welding samples for both TIG and laser welding before I decide?
Yes. DATO offers free welding sample testing for both process types. Provide your material, thickness, joint design, and quality requirements, and DATO's team will produce sample welds to help you compare process performance on your specific application before making a purchase decision. Contact DATO here to arrange your free sample test.
Ready to find the right welding process for your precision metal application?
Explore the DATO DT-HJR Robotic Laser Welding Machine Request a Free Welding Sample Test — TIG or Laser Get a Free Process Consultation from DATO's Engineering Team View All DATO Laser Welding Solutions
Shandong Dato Machinery Co., Ltd. — Laser Industry Leader Since 2007 info@datolaser.com | WhatsApp: +86-193-5317-3156 | www.datolaser.com
Related Blogs
-
 Why Manufacturers Are Buying Laser Welding Robots During The DATO LASER September Sourcing Sale 2026In 2026, manufacturers across the world are accelerating investments in laser welding robots, robotic laser welding systems, and other forms of smart manufacturing equipment to improve welding precision, reduce labor dependency, and build more efficient production lines.During the September SourcingBuyer's Guide
-
 DATO LASER Launches September Sourcing Sale with Up to 15% DiscountDATO LASER is proud to announce its September Sourcing Sale, running throughout the New Trade Festival period. This limited-time promotion offers customers up to 15% off on selected laser welding systems and CNC press brakes, along wBuyer's Guide
-
 Choosing a robotic welding system is not simply a choice between one robot brand and another. The right solution depends on your part size, weight, weld type, batch volume, changeover frequency, available floor space and required automation level.For many small and medium-sized metal fabrication shoBuyer's Guide
-
 Welding Positioner Types for Robotic Laser Welding: How to Choose the Right One for Your PartsMost buyers spend considerable time selecting the right robot arm and laser source for their robotic welding workstation. Far fewer give the same attention to the positioner — the component that holds, orieBuyer's Guide
